直驱 MK4 打 TPU 95A:PLA 五十分钟的件要打三小时二十五分
直驱机器打柔性料并不难,只是慢,而且失效模式永远一样——料在齿轮和熔化区之间拱起打折。这篇记录防止它的两个设置、柔性件为什么需要刻意过挤出,以及真实的耗时。
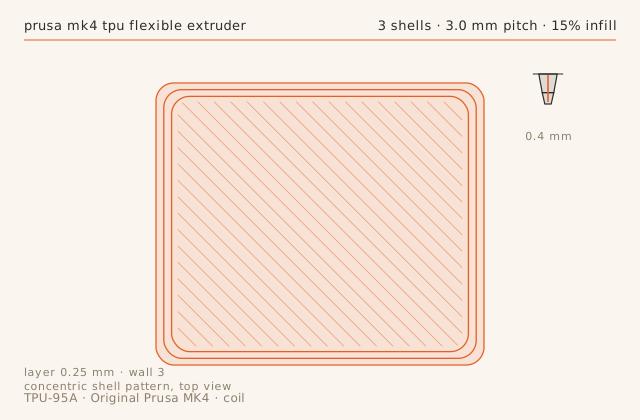
切片图按这条记录自己的切片参数画出来的。
打印记录
- 材料
- TPU-95A
- 喷嘴
- 0.4 mm
- 层高
- 0.25 mm
- 墙数
- 3
- 填充
- 15%
- 打印时长
- 3 小时 25 分
- 发布于
- 2026 年 9 月 26 日
让料打折的是背压
拿到柔性料,本能反应是把挤出机压臂调松。只有当料是被压扁时才管用;如果它是在齿轮上方拱起,问题是背压,不是夹持力。这次打印在 30 分钟、6 mm3/s 的体积流量上限下拱起。降到 3.5 mm3/s、外壁降到 20 mm/s,同一卷料一口气打完,一次都没卡。
一个不花钱的测试:在打印温度下用手把料推过喷嘴。如果明显费劲,说明体积流量上限定高了,任何挤出机设置都救不回来。
柔性件需要过挤出
TPU 出喷嘴之后会回弹,所以用跟 PLA 一样的倍率打出来的外壁更薄,与相邻走线之间会留缝。把挤出倍率从 1.00 提到 1.06,顶面就完全闭合了。这是少数几种「倍率大于 1.00 才是正确答案」的情况,而不是挤出机标定不准的症状。
同时把模型冷却从 70% 降到 40%,因为每一层在被吹冷之后才等来下一层,TPU 是焊不牢的。
速度是硬约束,不是偏好
在 PLA 里 50 分钟能打完的柔性护线圈,在这台机器上用 TPU 95A 打了 3 小时 25 分。大头是 20 mm/s 的外壁和 1000 mm/s2 的加速度上限。任何让它变快的设置,都会削掉你当初选 TPU 的理由。
围着它排计划,而不是跟它较劲。把所有柔性件排到同一次,因为准备工作完全一样,而中途卡一次就废掉整件。
什么时候偏小才是目标
护线圈 12 mm 内孔实测 11.42 mm,小了近 0.6 mm。对一个要夹住线缆的件来说,这正是想要的;把孔补偿到标称值,反而会做出一个会滑动的护线圈。先打一件偏小的,试装,只有夹得太紧时再加料。
凡是需要塞进刚性配合件的,方向正好相反:孔加 0.4 mm 再试。柔性件没有统一的公差方向。
失败链出了什么问题、当时怎么处理、最后是什么结果。
-
第几步 01
症状
Filament buckled between the extruder gears and the hotend at about 30 minutes into the print.
处理
Direct-drive path with very little gap, so the buckling had to be back-pressure: volumetric speed was 6 mm3/s. Dropped to 3.5 mm3/s and reduced the outer wall to 20 mm/s.
结果
Printed through. Total time went from an estimated 1 h 50 to 3 h 25, which is the real cost of flexible filament.
-
第几步 02
症状
Layer lines visible and gaps between perimeters on the top surface.
处理
TPU needs to be over-extruded relative to PLA. Raised the extrusion multiplier from 1.00 to 1.06 and dropped part cooling from 70 to 40 percent.
结果
Solid top surface with no gaps. Layer lines are still visible, which is unavoidable at 0.25 mm on a soft material.
尺寸复核
- 特征
- flexible grommet, inner bore
- 标称
- 12 mm
- 实测
- 11.42 mm-0.58
- 公差
- ± 0.2 mm
- 备注
- 0.58 mm undersized. Flexible material pulls inward as it cools; for a grommet that has to grip, undersize is a feature, not a defect.
切片档案
printer_model: Original Prusa MK4 0.4
layer_height: 0.25
perimeters: 3
infill: 15% gyroid
speed: 25 mm/s outer wall 20
accel: 1000 mm/s2
nozzle_temp: 235
bed_temp: 45
part_cooling: 40%
pressure_advance: 0.060
retraction: 0.2 mm at 15 mm/s, wipe on
max_volumetric_speed: 3.5 mm3/s
spool_holder: direct path, no reverse bowden restriction
沿用下来的做法
- 齿轮上方拱起是背压问题:降体积流量到 3.5 mm3/s,不是调压臂。
- TPU 95A 用 1.06 挤出倍率,把外壁之间的缝隙闭上。
- 模型冷却取 40%;70% 会在下一层到来之前把每层吹冷。
- PLA 50 分钟的件在 20 mm/s 外壁下要打 3 小时 25 分;柔性件集中排产。
结论
TPU 95A 在这台机器上以 3.5 mm3/s 的参数档可稳定复现。它仍然是批量材料,不是日常材料。
同一台机器上还有 Original Prusa MK4
-
打印日志
Nextruder 冷拔:三次拉丝,和那些看着像欠挤出的麻点
壁厚正确却出现表面麻点,这大概率不是流量问题,是污染。这篇记录在 MK4 的 Nextruder 喷嘴上有效的冷拔流程、为什么温度比手法更关键,以及大多数人跳过的那一步排废。
- 材料PLA
- 喷嘴0.4 mm
- 层高0.2 mm
- 打印时长1 小时 1 分
- 失败链2
-
打印日志
MMU3 换色:排废量比参数档里其他任何东西都重要
MK4 多色打印的失败只有两种——过渡脏和拖丝——而两者都是排废与擦嘴问题,不是模型或切片问题。这篇记录一块换色 13 次的 60 mm 铭牌、最终做出干净分界的排废量,以及每次擦嘴多花的 9 秒。
- 材料PLA
- 喷嘴0.4 mm
- 层高0.2 mm
- 打印时长3 小时 56 分
- 失败链2
-
打印日志
MK4 的有机支撑:PETG 能用的 Z 间隙不是 PLA 能用的那个
树状支撑看着像个已经解决的问题,直到你换材料。PETG 在 0.15 mm 间隙下会自己焊起来,于是 PLA 的标准间隙直接把支撑粘死在件上。这篇记录让 PETG 支撑能用手掰下来的间隙与接触面设置,以及让高树不倒的稳定性修法。
- 材料PETG
- 喷嘴0.4 mm
- 层高0.2 mm
- 打印时长2 小时 52 分
- 失败链2