Ender-3 V3 KE 的 PETG 参数档:别再跟原厂设置较劲
KE 出厂的挤出倍率、回抽距离和床温都是为 PLA 设的,而这三项对 PETG 全部不利。这套参数换掉了其中五项,数值都来自这台机器的实测,而不是通用的 PETG 起始值。
切片图按这条记录自己的切片参数画出来的。
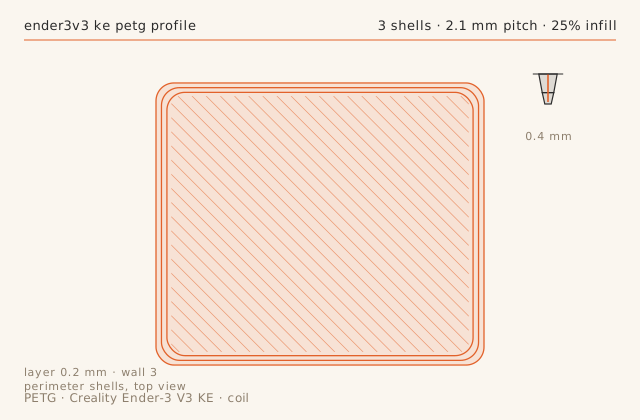
打印记录
- 材料
- PETG
- 喷嘴
- 0.4 mm
- 层高
- 0.2 mm
- 墙数
- 3
- 填充
- 25%
- 打印时长
- 1 小时 48 分
- 发布于
- 2026 年 8 月 31 日
第一个要改的就是原厂倍率
创想三维默认的 1.00 挤出倍率打出 0.45 mm 壁厚,目标是 0.42 mm,40 mm 方块涨到 40.16 mm。降到 0.95 后壁厚 0.41 mm、方块 39.91 mm。KE 的直驱 Sprite 挤出机有效熔程比 bowden 结构短,多余压力被导料管吸收得更少,所以过挤出的可见后果来得更早。
判断依据是顶部外壁与顶面填充交界处的凸棱:多挤出来的材料没有地方可去,只能堆在外壁内侧。看到这个就先改倍率,别的都往后放,因为改温度只会让表面变花而不会让凸棱消失。
这里的回抽要比现代直驱更长
这台机器上止住拉丝的值是 1.4 mm,而 MK4 上是 0.8 mm。Sprite 挤出机熔程更长、喷嘴离送料齿轮更远,需要拉回更多料才能把尾巴扯断。低于 1.2 mm 时每次长行程都会拉丝;到 1.8 mm,被拖进冷区的料把喷嘴堵了。
可用窗口大约只有 0.6 mm 宽。以 0.2 mm 为步长改,每改一次打一座拉丝塔,不要靠猜。
床温和板材清洁度是同一个问题
最初三次打印都中途脱落。原因不是温度设置,而是板面:用异丙醇擦其实只是在把皮肤油脂抹匀,并没有去掉。热水加洗洁精加厨房纸解决之后,床温从 75 提到 80 C,连续十次没再脱落。85 C 时首层被压出象脚,需要 0.4 mm 倒角才能消掉。
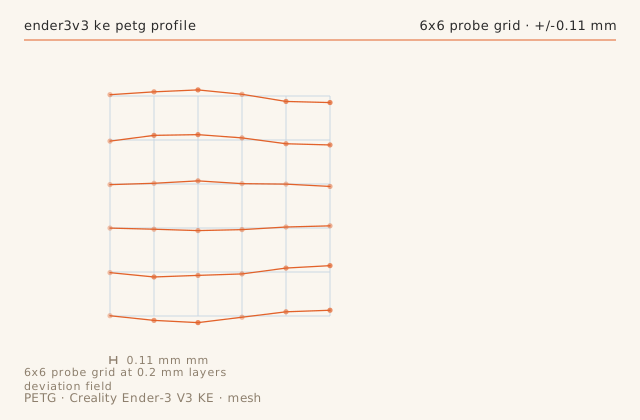
KE 的自动网格也比床面更平的机器更重要:原装板峰谷差 0.11 mm,每次 PETG 打印前重跑一次 6x6 网格,那 90 秒值得花。
这台机器上不要压榨外壁速度
KE 标称速度很高,运动系统也确实能跑到,但它是床身移动结构、带着运动质量,外壁跑到 90 mm/s 时件上出现了 input shaper 也压不干净的拐角振纹。60 mm/s 下拐角干净,典型 40 mm 件 108 分钟,而 90 mm/s 约 85 分钟。
填充跑 120 mm/s 没有任何可见代价。为省那 23 分钟去压榨外壁,不值得拿表面来换。
失败链出了什么问题、当时怎么处理、最后是什么结果。
-
第几步 01
症状
Parts detached from the textured PEI sheet mid-print on the first three attempts.
处理
Washed the sheet with hot water and dish soap rather than IPA, then ran a fresh 6x6 bed mesh and raised the bed to 80 C.
结果
Ten consecutive prints with full adhesion. IPA alone had been spreading the skin oils around rather than removing them.
尺寸复核
- 特征
- 40 mm PETG calibration block
- 标称
- 40 mm
- 实测
- 39.91 mm-0.09
- 公差
- ± 0.1 mm
- 备注
- 0.95 multiplier keeps the block under 40 mm. The KE's stock multiplier of 1.00 grows PETG parts by about 0.4 percent at this size.
参数扫描
| 参数 | 试过 | 选定 | 理由 |
|---|---|---|---|
| Extrusion multiplier | 0.92 / 0.94 / 0.95 / 1.00 | 0.95 | 0.95 gave a 0.41 mm wall and a 39.91 mm block; 1.00 gave a 0.45 mm wall, ridges and a 40.16 mm block. |
| Nozzle temperature | 225 / 230 / 235 / 242 C | 235 C | 225 C caused layer separation on a 3 mm wall; 242 C produced heavy stringing on the stock 1.4 mm retraction. |
| Retraction | 1.0 / 1.2 / 1.4 / 1.8 mm | 1.4 mm | The KE's Sprite extruder has a longer bowden-free path than the MK4. 1.0 and 1.2 left strings; 1.8 pulled molten material into the cold zone. |
| Bed temperature | 70 / 75 / 80 / 85 C | 80 C | At 70 C the first layer lifted at the corners of a 150 mm part; 85 C caused elephant-footing that needed a 0.4 mm chamfer. |
| Perimeter speed | 40 / 60 / 90 / 120 mm/s | 60 mm/s | The KE's bed is not rigid enough for high outer wall speeds; at 90 mm/s the part showed corner ringing that the input shaper could not fully remove. |
切片档案
# LayerLog PETG profile v2 — Creality Ender-3 V3 KE, stock 0.4 nozzle
# Creality OS (Klipper) — pressure advance via the printer.cfg, not the slicer
nozzle_temp: 235
nozzle_temp_first_layer: 238
bed_temp: 80
layer_height: 0.20
first_layer_height: 0.28
perimeters: 3
perimeter_speed: 60
infill_speed: 120
solid_infill_speed: 90
travel_speed: 250
accel: 3000
pressure_advance: 0.046
retraction: 1.4 mm at 30 mm/s, wipe on
max_volumetric_speed: 10 mm3/s
extrusion_multiplier: 0.95
seam_position: rear
z_hop: 0.4 mm
bed_mesh: 6x6 auto, run before every PETG print
沿用下来的做法
- KE 上挤出倍率设 0.95;原厂 1.00 会把 PETG 件做大 0.4% 左右。
- 回抽用 1.4 mm,而 MK4 上是 0.8 mm——Sprite 的熔程更长。
- PEI 板用热水加洗洁精洗;只用异丙醇等于把油脂抹匀。
- 这台床身移动机型外壁保持 60 mm/s;只有填充能跑 120 mm/s。
结论
这是 KE 上 40 mm 件 108 分钟的 PETG 工作参数档。每次打印前重跑床面网格,并保持板面清洁。
同一台机器上还有 Creality Ender-3 V3 KE
-
打印日志
给 KE 换高流量热端:22 mm3/s,以及必须重新推导的压力提前量
换高流量热端把 KE 的体积流量上限从约 11 提到 22 mm3/s,典型件从 108 分钟缩到 67 分钟。代价是它让此前所有压力提前量数值全部失效,这篇大半时间讲的就是这件事。
- 材料PLA
- 喷嘴0.4 mm
- 层高0.2 mm
- 打印时长1 小时 7 分
- 失败链2
-
打印日志
KE 的 Z 向横纹:先是 8 mm 周期,然后是 2 mm 周期,两种不同的解法
Z 向横纹是有周期的,而周期在你动手之前就能告诉你原因。这篇处理同一台机器上的两种横纹——一种对应丝杠旋转周期、一种对应螺纹螺距——并说明为什么前者必须机械修,后者只能软件补。
- 材料PLA
- 喷嘴0.4 mm
- 层高0.2 mm
- 打印时长58 分钟
- 失败链2
-
调校档案
KE 原装挤出机打 TPU 95A:3 小时 44 分,以及唯一那个拱起的位置
KE 的 Sprite 挤出机是直驱,这让柔性料「可行」而不是「容易」。这套参数围绕一个机器真能扛住的 3.0 mm3/s 上限来搭,并写清每次失败都失败在同一个位置。
- 材料TPU-95A
- 喷嘴0.4 mm
- 层高0.24 mm
- 打印时长3 小时 44 分
- 失败链2