MK4 的有机支撑:PETG 能用的 Z 间隙不是 PLA 能用的那个
树状支撑看着像个已经解决的问题,直到你换材料。PETG 在 0.15 mm 间隙下会自己焊起来,于是 PLA 的标准间隙直接把支撑粘死在件上。这篇记录让 PETG 支撑能用手掰下来的间隙与接触面设置,以及让高树不倒的稳定性修法。
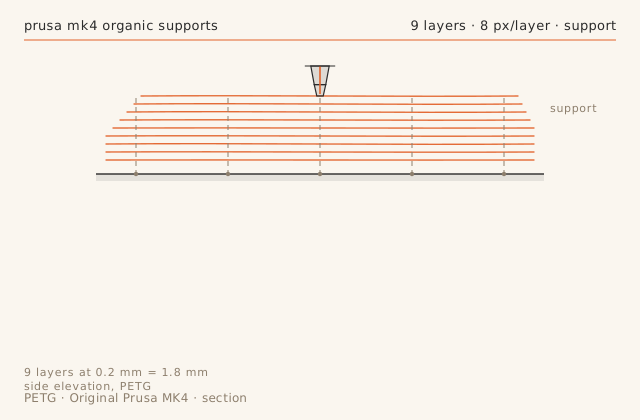
切片图按这条记录自己的切片参数画出来的。
打印记录
- 材料
- PETG
- 喷嘴
- 0.4 mm
- 层高
- 0.2 mm
- 墙数
- 3
- 填充
- 25%
- 打印时长
- 2 小时 52 分
- 发布于
- 2026 年 9 月 15 日
Z 间隙是跟材料走的
0.15 mm 对 PLA 没问题,对 PETG 太小。原因是 PETG 自粘更凶,0.15 mm 下接触面和模型表面仍在可粘接范围内。把间隙提到 0.20 mm 就解决了粘连;留下的表面略糙一些,但那是没被刀碰过的表面,这个交换值得做。
这是仅次于「完全不用接触面」的第二常见支撑错误。同一个模型要打两种材料,就存两套支撑预设,而不是一套。
让接触面有自己的厚度
0.2 mm 层高下,一层接触面不够:单层接触面是厚度不均的局部层,有的地方粘住、有的地方没粘。三层接触面形成一块刚性片,整体脱离,留下的表面一致性也好。
多数切片软件里接触面还会打得更慢,这是对的。被支撑的那一面决定了模型的观感,值得多花这个时间。
高树需要更宽的底
支撑在 60% 高度处脱落,因为又高又轻的结构下面底座太窄。解法是两个几乎不花时间的设置:只给支撑加底筏,以及把分叉角从 50 度降到 45 度。角度更小让树底部更宽,也更抗喷嘴每次行程给它的那点横向推力。
不要用加大支撑密度来治这个问题。密度增加的是整棵树的质量,顶端也一起变重,只会更糟。
把拆除时间也算进去
0.15 mm 间隙带来的支撑面更好——下垂 0.06 mm 对 0.12 mm——但拆除从手掰约 20 秒变成用刀几分钟,还留下可见划痕。对于功能支架,手掰版本即使底面更糙也胜出。
两个数字都要记下来。一套二十件的批量里,多花四分钟拆除的支撑设置,代价超过它省下的打印时间。
失败链出了什么问题、当时怎么处理、最后是什么结果。
-
第几步 01
症状
Support fused to the model on the flat underside, requiring a knife and leaving white stress marks.
处理
Z-gap was 0.15 mm with PETG, which bonds to itself too well at that distance. Raised to 0.20 mm and increased support interface layers from 1 to 3 so the interface had its own structure to break away from.
结果
Supports snap off by hand. Surface underneath is slightly rougher but has no knife marks.
-
第几步 02
症状
The whole support tree detached and fell over mid-print at 60 percent height.
处理
Organic supports had a narrow base on a tall, light part. Added a 6 mm brim to the support only, and lowered the support branch angle from 50 to 45 degrees.
结果
Second attempt completed. Support tree was stable despite a 4 mm mid-print wobble.
尺寸复核
- 特征
- overhang surface flatness under supported region
- 标称
- 0 mm
- 实测
- 0.12 mm+0.12
- 公差
- ± 0.08 mm
- 备注
- 0.12 mm of sag on the supported overhang with a 0.20 mm z-gap. Reducing the gap to 0.15 mm improved it to 0.06 mm but doubled the removal time.
切片档案
printer_model: Original Prusa MK4 0.4
layer_height: 0.20
perimeters: 3
infill: 25% grid
support: organic, 0.20 mm z-gap
support_angle: 55 deg
support_interface: 3 layers
speed: 120 mm/s outer wall 60
accel: 4000 mm/s2
nozzle_temp: 240
bed_temp: 85
part_cooling: 50%
pressure_advance: 0.042
沿用下来的做法
- PETG 支撑用 0.20 mm Z 间隙;0.15 mm 会把接触面焊到件上。
- 三层接触面能整片脱离,一层不行。
- 高支撑树加只给支撑的底筏,并把分叉角降到 45 度。
- 0.15 mm 间隙下垂只有 0.06 mm,但把 20 秒的拆除变成几分钟。
结论
PETG 支撑预设定为 0.20 mm 间隙 + 三层接触面。底面偏糙对功能件可接受,对外观件不可接受。
同一台机器上还有 Original Prusa MK4
-
打印日志
Nextruder 冷拔:三次拉丝,和那些看着像欠挤出的麻点
壁厚正确却出现表面麻点,这大概率不是流量问题,是污染。这篇记录在 MK4 的 Nextruder 喷嘴上有效的冷拔流程、为什么温度比手法更关键,以及大多数人跳过的那一步排废。
- 材料PLA
- 喷嘴0.4 mm
- 层高0.2 mm
- 打印时长1 小时 1 分
- 失败链2
-
打印日志
MMU3 换色:排废量比参数档里其他任何东西都重要
MK4 多色打印的失败只有两种——过渡脏和拖丝——而两者都是排废与擦嘴问题,不是模型或切片问题。这篇记录一块换色 13 次的 60 mm 铭牌、最终做出干净分界的排废量,以及每次擦嘴多花的 9 秒。
- 材料PLA
- 喷嘴0.4 mm
- 层高0.2 mm
- 打印时长3 小时 56 分
- 失败链2
-
打印日志
直驱 MK4 打 TPU 95A:PLA 五十分钟的件要打三小时二十五分
直驱机器打柔性料并不难,只是慢,而且失效模式永远一样——料在齿轮和熔化区之间拱起打折。这篇记录防止它的两个设置、柔性件为什么需要刻意过挤出,以及真实的耗时。
- 材料TPU-95A
- 喷嘴0.4 mm
- 层高0.25 mm
- 打印时长3 小时 25 分
- 失败链2